The welding method you choose has a direct impact on the quality of your custom metal work. This guide explains MIG, TIG, and arc welding, and how to match the right process to your project.
When you commission custom metal work, you are not just specifying a material and a shape. You are also, whether you realise it or not, specifying a manufacturing process. And the welding method your fabricator uses will directly affect the strength, appearance, and longevity of your finished part.
Most buyers do not think about this until something goes wrong. So this guide explains the main welding processes, what each one delivers, and how to make sure your fabricator is using the right method for the job.
Why Welding Method Matters More Than Most Buyers Realise
A weld is not just a join. It is a metallurgical bond created by melting two pieces of metal together, sometimes with a filler material added. The quality of that bond depends on the process used, the skill of the welder, the material being joined, and the conditions in which the weld is made.
Get it right, and the weld is as strong as the parent metal. Get it wrong, and you have a weak point that can fail under load, crack under stress, or corrode faster than the surrounding material.
In custom metal work, welds are often structural. They carry loads, transfer forces, and hold assemblies together. Choosing the wrong process, or working with a fabricator who applies a process carelessly, puts the entire fabrication at risk.
The Three Main Welding Processes Used in Custom Metal Fabrication
MIG Welding
MIG welding, or Metal Inert Gas welding, is the most widely used process in general fabrication. It uses a continuously fed wire electrode and a shielding gas to protect the weld pool from contamination.
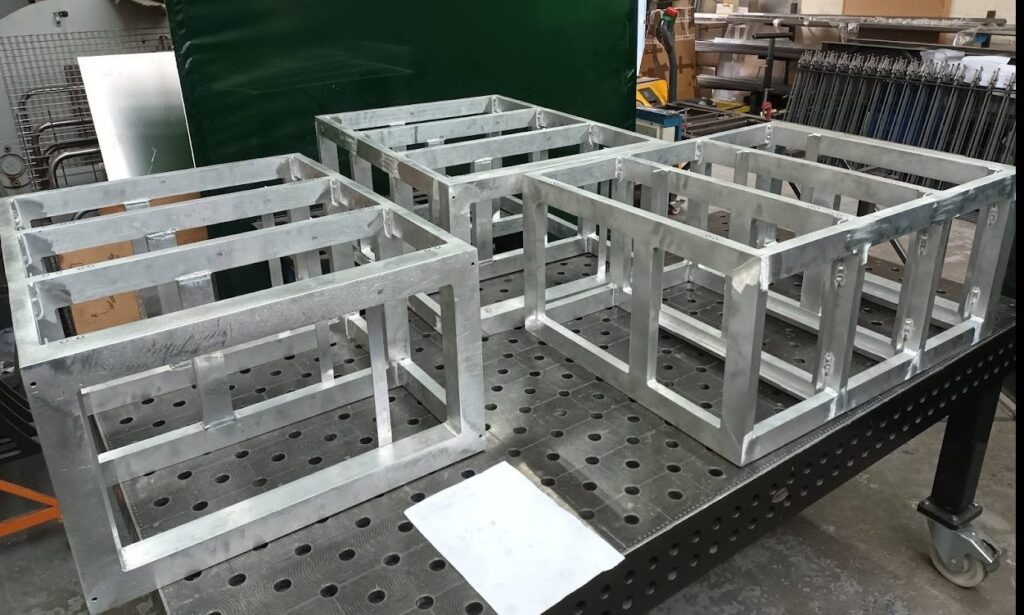
MIG welding is fast. It suits mild steel and aluminium well, and it can handle a wide range of material thicknesses. For most structural custom metal work, MIG welding is the right choice.
The finished weld has a slightly raised bead. On structural work, this is perfectly acceptable. On visible or decorative fabrications, the bead may need grinding back to achieve a cleaner appearance.
MIG welding is also well suited to batch production. If your custom metal work involves repeated components, MIG welding keeps cycle times down without sacrificing joint integrity.
TIG Welding
TIG welding, or Tungsten Inert Gas welding, uses a non-consumable tungsten electrode and a separate filler rod fed by hand. The welder has precise control over the heat input and the weld pool at all times.
This makes TIG welding significantly slower than MIG. However, it produces a far superior finish. The weld bead is neat, consistent, and often requires little or no post-weld finishing.
TIG welding is the preferred method for stainless steel custom metal work. Stainless is sensitive to heat distortion, and TIG’s controlled heat input reduces the risk of warping. It also preserves the corrosion-resistant oxide layer on stainless steel far better than MIG.
For custom metal work where appearance matters, such as architectural features, food-grade equipment, or visible structural elements, TIG welding is worth the additional time and cost.
Arc Welding
Arc welding, also called MMA or stick welding, uses a consumable electrode coated in flux. It is the most versatile process in terms of environment. It works outdoors, in windy conditions, and on materials that are not perfectly clean.
Arc welding is less precise than MIG or TIG. It is harder to achieve a consistent finish, and it produces more spatter. However, it suits heavy structural work and site-based fabrication well.
For on-site custom metal work, such as installing steel structures or making field repairs, arc welding is often the practical choice even when MIG or TIG would be preferred in a workshop setting.
How Material Type Affects Welding Method Choice
The material you specify for your custom metal work largely determines which welding process is appropriate.
Mild Steel
Mild steel is the most forgiving material to weld. All three processes work on mild steel. MIG welding is the standard choice for most mild steel custom fabrications. Arc welding suits site work and heavy plate. TIG welding is used when a high-quality finish is required.
Stainless Steel
Stainless steel requires more care. TIG welding is strongly preferred because it minimises heat input and protects the surface finish. MIG welding on stainless is possible but carries a higher risk of discolouration and heat distortion if not handled carefully.
For food-grade or pharmaceutical custom metal work, TIG welding is almost always specified. The smooth, continuous weld bead is easier to clean and less likely to harbour bacteria.
Aluminium
Aluminium is more challenging to weld than steel. It conducts heat quickly, which can lead to burn-through if heat input is not controlled. MIG welding works well on aluminium with the correct wire and shielding gas. TIG welding on aluminium produces excellent results but demands a high level of operator skill.
If your custom metal work involves aluminium, make sure your fabricator has genuine experience with it. Not all fabricators weld aluminium regularly, and inexperience shows quickly in the finished result.
The Role of Welder Skill and Procedure
Welding method is only part of the picture. The skill and qualification of the welder matters just as much.
A well-qualified welder following a documented welding procedure will consistently produce sound joints. An unqualified welder using the correct process can still produce weak or defective welds that pass visual inspection but fail under load.
When placing custom metal work orders, it is reasonable to ask whether your fabricator operates a documented quality management system. ISO 9001 certified fabricators maintain controlled welding procedures, and they track welder qualifications as part of their quality framework. This gives you confidence that the welds in your finished parts meet the required standard, not just on one job, but consistently.
What to Look for in a Finished Weld
When your custom metal work is delivered, a basic visual check is worth doing before it goes into service.
Look for consistent weld bead width along the joint. Variation in bead width can indicate inconsistent travel speed or heat input. Check for porosity, which shows as small holes or pits in the weld surface. These indicate gas contamination during welding and can weaken the joint.
Look also for undercutting, a groove along the edge of the weld where the parent metal has been eroded. Undercutting reduces the cross-section of the joint and creates a stress concentration point.
A clean, consistent weld with no visible defects is a good indicator that the fabrication process was well controlled from start to finish.
Choosing a Fabricator Who Gets This Right
The welding method used in your custom metal work should not be an afterthought. It should be part of the conversation when you place your order.
At Ashland Engineering in Milton Keynes, both MIG and TIG welding are available in-house. The team matches the process to the material and application rather than defaulting to the fastest option. Whether your project requires mild steel structural fabrication, stainless steel food-grade components, or precision aluminium parts, the right welding process is applied from the start.
Ashland Engineering holds ISO 9001 certification, which means quality is built into every stage of production, including welding. Customers across Buckinghamshire, Northamptonshire, Bedfordshire, and the wider UK can rely on consistent, documented, and quality-controlled fabrication.
To discuss your custom metal work requirements, contact the team at sales@ashlandengineering.co.uk or call 01908 382 599.